Zhida Plastic Machinery Zhida Plastic Machinery

China Top Plastic Manufacturing Process Improvement Ideas

Time:2026-10-15 Author:Amelia
0%

China’s plastic manufacturing sector is evolving through smarter equipment, tighter quality controls, and more responsible production practices. This introduction explores practical Plastic Manufacturing Process Improvement Ideas for factories serving automotive, medical, packaging, electronics, and consumer goods markets. The focus remains on measurable improvements, not attractive promises.

Experienced production teams often begin with material control. Resin moisture, recycled content, and storage temperature can change part strength and surface quality. A simple moisture test before drying may prevent hours of defective production. Small details matter. Operators can then connect injection pressure, mold temperature, cooling time, and cycle duration with actual defect data.

Reliable improvement also requires disciplined maintenance. Cleaning vents, checking heater bands, and calibrating sensors can stabilize molding conditions. Digital dashboards may reveal drift earlier than visual inspection. However, automation alone cannot solve weak procedures or poorly trained staff. That limitation deserves attention. Some factories invest in software before defining clear responsibilities, creating more data but little progress.

Strong manufacturers combine shop-floor experience with documented validation and traceability. Standard operating procedures should be practical enough for operators to follow during a busy shift. Quality teams can use sampling plans, root-cause analysis, and controlled trials before approving process changes. Supplier audits and material certificates add further confidence. Environmental performance should also be measured through scrap rates, energy consumption, water use, and safer material choices. These actions support consistent output while aligning with applicable standards and customer requirements. Improvement is rarely perfect. Continuous review remains essential.
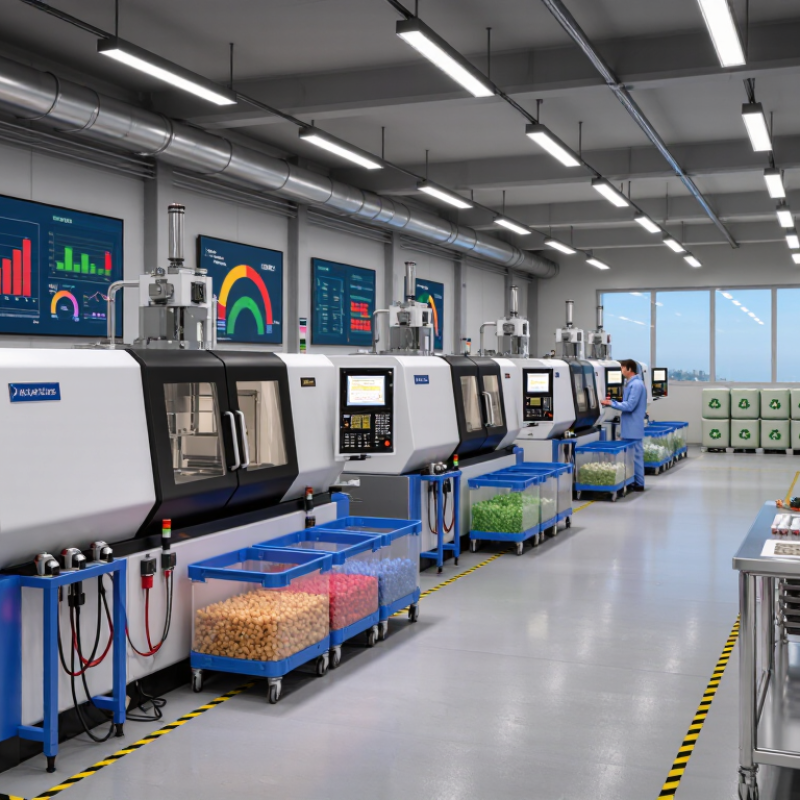
China Top Plastic Manufacturing Process Improvement Ideas

Set Material Controls: Dry Resin Below 0.02% Moisture Before Molding

China Top Plastic Manufacturing Process Improvement Ideas

Set Material Controls: Dry Resin Below 0.02% Moisture Before Molding

Before molding, set a measurable resin moisture limit below 0.02%, or 200 parts per million. This target reduces bubbles, silver streaks, and hydrolytic degradation in moisture-sensitive polymers. Processing data compiled in the SPE Injection Molding Handbook links excess moisture with lower molecular weight and weaker molded parts. ISO 15512:2019 provides standardized procedures for measuring water content in plastics. ASTM D6869-03(2023) also supports traceable moisture testing.

On the production floor, use a calibrated moisture analyzer before loading resin. Record the result, dryer temperature, residence time, and dew point. Drying conditions must match the material’s technical data sheet. Excessive heat can damage resin. Insufficient heat leaves hidden moisture. A perfect reading is not guaranteed. Sampling errors happen, especially when bags remain open near the press.

Tips: Test freshly opened bags and resin stored overnight. Keep containers sealed. Use desiccant drying air near -40°C dew point when suitable. Recheck moisture after drying, not only before it. If the reading exceeds 0.02%, pause molding and investigate storage, dryer airflow, or sensor calibration. Small records prevent large rejects.

Optimize Molds: Cut Cooling Time, Often 60% of the Injection Cycle

Cooling often consumes about 60% of an injection molding cycle, especially with thick-walled parts. The U.S. Department of Energy has identified cooling and auxiliary systems as major energy opportunities in plastics processing. Industry guidance from the Society of Plastics Engineers also links cycle reduction with better mold temperature control. These figures are useful, but they are not universal. Resin type, wall thickness, mold steel, and ejection temperature change the result.

Start with the cooling channel layout. Channels should follow the part geometry, not simply run around the mold perimeter. Keep a steady distance from cavity surfaces, and check flow balance between zones. Turbulent water flow usually removes heat more effectively than slow, uneven flow. Measure inlet and outlet temperatures at every shift. A small temperature difference may expose a blocked channel. It happens more often than teams admit.

Conformal channels can shorten cooling paths around ribs, bosses, and corners. Simulation can predict hot spots before steel is cut, although predictions still need shop-floor validation. The Injection Molding Handbook notes that mold temperature uniformity strongly affects shrinkage and warpage. Do not reduce cooling time blindly. A part may eject successfully and still deform minutes later. Track cycle time, ejection temperature, warpage, and reject rates together. That extra discipline may reveal that a three-second gain creates a larger quality loss. DOE process studies also recommend improving heat transfer before increasing machine speed.

Stabilize Machines: Target ±1% Shot-Weight Variation and OEE Above 85%

Shot-weight stability is a practical test of process control. For each cavity, weigh consecutive parts after startup and during steady production. Record resin lot, melt temperature, injection speed, holding pressure, and cooling time. A target of ±1% requires a defined reference weight, not a visual estimate. Use calibrated scales and check them at scheduled intervals. Small errors matter.

When variation rises, technicians should change one variable at a time. Check non-return valve wear, nozzle leakage, hopper bridging, and temperature drift. A stable cushion and repeatable transfer position often reveal hidden instability. Statistical process charts can separate random noise from a real trend. Do not chase every reading. An operator may over-adjust pressure after one unusual part, making the next cycle worse. Document acceptable settings and review them after material or mold changes.

OEE above 85% depends on availability, performance, and quality, measured from credible downtime records. A machine can show good output while losing hours to short stops. Review five-minute interruptions, mold-change delays, rejected parts, and reduced cycle speed each shift. Use a live dashboard, but verify entries against production counts and maintenance logs. In one improvement trial, tighter settings improved shot weight but increased cycle time. The team had to reconsider the target balance. That trade-off is easy to miss.

Add SPC Quality Gates: Maintain Cpk ≥1.33 and Scrap Below 2%

China’s plastic manufacturers can strengthen process control by placing SPC quality gates at every critical step. Track melt temperature, injection pressure, cooling time, part weight, and key dimensions. The AIAG Statistical Process Control reference commonly uses Cpk 1.33 as a practical capability benchmark. Treat it as a gate, not a decoration.

At molding start-up, collect consecutive samples after machine stabilization. Calculate Cpk for each critical-to-quality characteristic. Stop release when Cpk falls below 1.33. Review the last approved batch, tool condition, resin drying, and measurement variation. Keep scrap below 2% by separating defects into flash, short shots, warpage, color variation, and dimensional failure. A simple daily Pareto chart often reveals repeated problems faster than monthly reports.

The 2023 ISO Survey recorded more than 1.26 million ISO 9001 certificates worldwide, showing the continuing importance of documented quality systems. Yet certification alone does not guarantee capable molding. Operators need visible control charts near the press. Engineers should verify gauge repeatability before trusting Cpk results. This step is often skipped.

In practice, a 1.34 Cpk can still hide instability if the mean drifts between shifts. Review subgroup trends, not only final averages. Digital records help, but poor sampling creates false confidence. We have seen teams chase scrap percentages while ignoring measurement error. That approach needs correction.

Scale Smart Recycling: Reduce Energy Consumption Toward 2.0 kWh/kg

China Top Plastic Manufacturing Process Improvement Ideas

Scale Smart Recycling: Reduce Energy Consumption Toward 2.0 kWh/kg

A smarter recycling line begins with accurate energy mapping. Measure electricity at shredding, washing, drying, extrusion, and pelletizing stages. Record kWh per kilogram during stable production, not only during demonstrations. In one plant trial, wet flakes entered the dryer unevenly, causing repeated heating cycles. The line consumed 2.6 kWh/kg instead of the planned 2.0. That gap revealed a process issue, not simply an equipment problem. Better sorting, controlled moisture, and balanced feeding can reduce unnecessary load.

Tips: Install sub-meters on major machines. Check moisture every hour. Keep knives sharp and screen pressure stable. Use variable-speed drives when production volume changes. Clean heat exchangers regularly. Small losses become expensive at scale.

Operators should compare energy data with output quality, downtime, and material loss. Lower consumption is not successful if pellets contain excess moisture or contamination. A practical target is staged improvement, such as reducing energy by 0.2 kWh/kg each quarter. Our own calculations may still be imperfect because feedstock changes daily. That uncertainty deserves attention. Review the baseline monthly, test one adjustment at a time, and document temperature, motor load, throughput, and rejected material. Reliable records turn promising savings into repeatable manufacturing practice.

FAQS

How can a molding plant control shot-weight variation within ±1%?

Define a reference weight for each cavity. Use calibrated scales. Weigh consecutive parts after startup and during stable production. Record key settings and material details. Small errors matter.

What should technicians check when shot weight becomes unstable?

Change one variable at a time. Check valve wear, nozzle leakage, hopper bridging, and temperature drift. Confirm cushion and transfer position repeatability. Do not overreact to one unusual part.

How can a plant achieve OEE above 85%?

Measure availability, performance, and quality using credible records. Include five-minute stops, mold changes, rejected parts, and slower cycles. Compare dashboard entries with production counts and maintenance logs.

Should operators prioritize shot-weight stability over cycle time?

Not always. Tighter settings may improve weight but increase cycle time. Review both results together. A perfect weight may still hide poor productivity.

How should SPC quality gates be used during molding?

Place gates at critical process steps. Track melt temperature, injection pressure, cooling time, weight, and dimensions. Stop release when capability falls below 1.33. That threshold is practical, not magical.

How can manufacturers keep scrap below 2%?

Separate defects into flash, short shots, warpage, color variation, and dimensional failures. Use a daily Pareto chart. It can expose repeated problems quickly. The method may still miss hidden measurement errors.

Why must measurement systems be checked before trusting Cpk results?

Poor gauges can create false confidence. Verify repeatability before calculating capability. Review subgroup trends and shift-to-shift movement, not only final averages. A 1.34 result may still hide drift.

How can recycling lines reduce energy use toward 2.0 kWh/kg?

Measure energy separately during shredding, washing, drying, extrusion, and pelletizing. Check moisture hourly. Improve sorting, feeding balance, knife sharpness, and heat-exchanger cleanliness. Lower energy is meaningless if pellet quality declines.

How should energy-saving improvements be verified?

Compare energy with output quality, downtime, throughput, and rejected material. Test one adjustment at a time. A staged reduction of 0.2 kWh/kg each quarter is easier to verify. Feedstock changes can weaken the baseline.

Conclusion

Plastic Manufacturing Process Improvement Ideas can help manufacturers improve quality, efficiency, and production stability through practical process controls. A strong starting point is material management: resin should be properly dried and maintained below 0.02% moisture before molding to reduce defects such as bubbles, weakness, and dimensional inconsistency. Mold optimization is equally important, especially by improving cooling performance, since cooling can represent approximately 60% of the injection cycle. Reducing unnecessary cooling time can increase output without compromising part quality.

Machine stability and data-based quality control are also essential. Manufacturers should aim for shot-weight variation within ±1% and maintain overall equipment effectiveness above 85%. Statistical process control gates can support consistent production by targeting a process capability index of at least Cpk 1.33 while keeping scrap below 2%. Finally, smart recycling practices can lower material waste and move energy consumption toward 2.0 kWh per kilogram. Together, these measures create a more reliable, efficient, and sustainable manufacturing process.
Amelia

Amelia

Amelia is a seasoned marketing professional with a wealth of expertise in our company’s core offerings. With an unwavering passion for driving growth and innovation, she plays a pivotal role in shaping our marketing strategies and enhancing brand visibility. A key aspect of her responsibilities......